


500,000+
Managed products

500,000+
Managed products
Warranty
12 months for all products
Express delivery
Always and everywhere
4,9
Average reviews
Everywhere
Worldwide support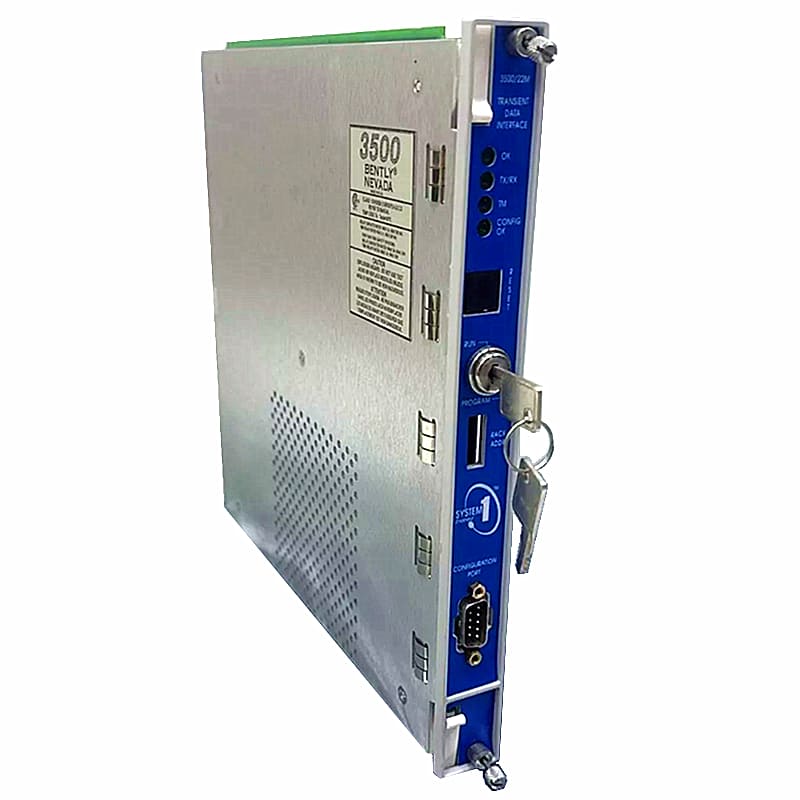
3500 System, Proximity Probes, Sensors & Transducer Systems, AHM Sensors, Accelerometers, etc.
ControLogix, CompactLogix, Flex I/O, etc.
DCS 800xA, AC500, S700, S800, S900, etc.
Experion PKS C300, HC900, etc.
Simatc S7-200, S7-400, S7-1200, S7-1500, HMI, etc.
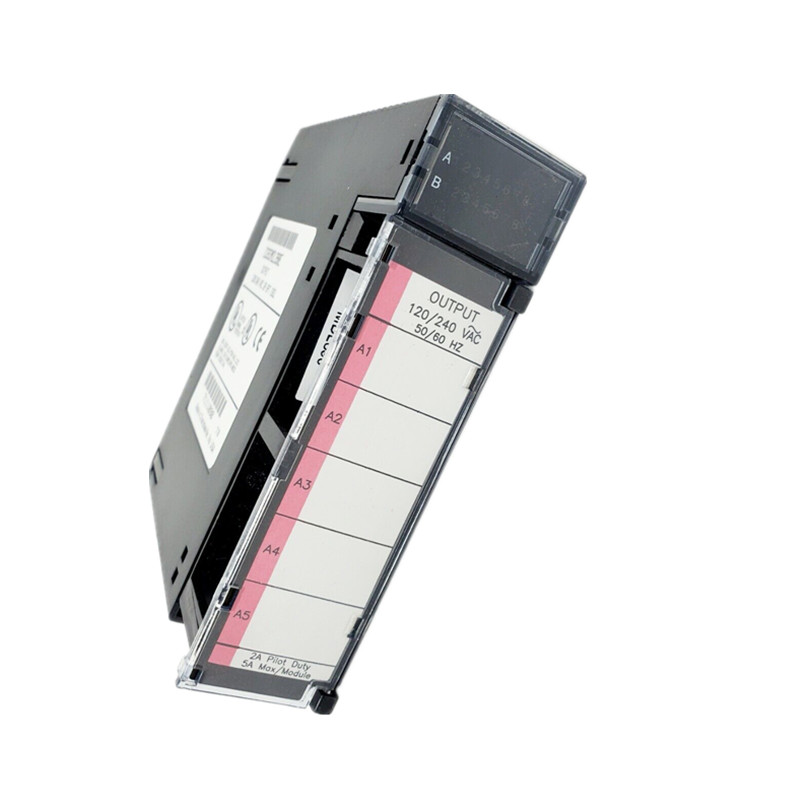
90-70, 90-30, PACSystems* RX7i, RX3i, VersaMax PLC, etc.
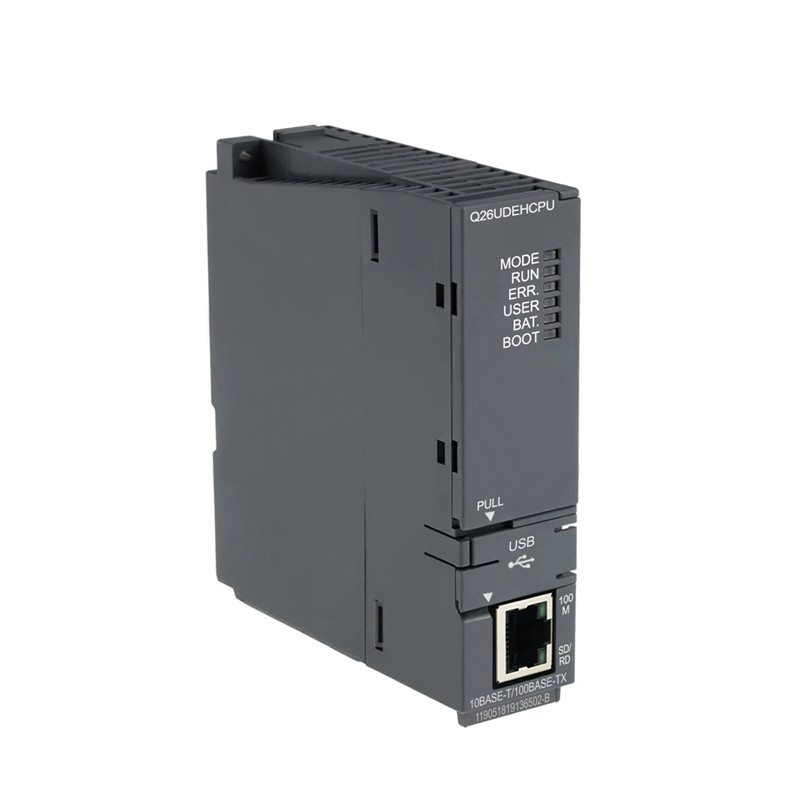
MELSEC-Q Series, MELSEC-F Series, MELSEC iQ-F Series, etc.
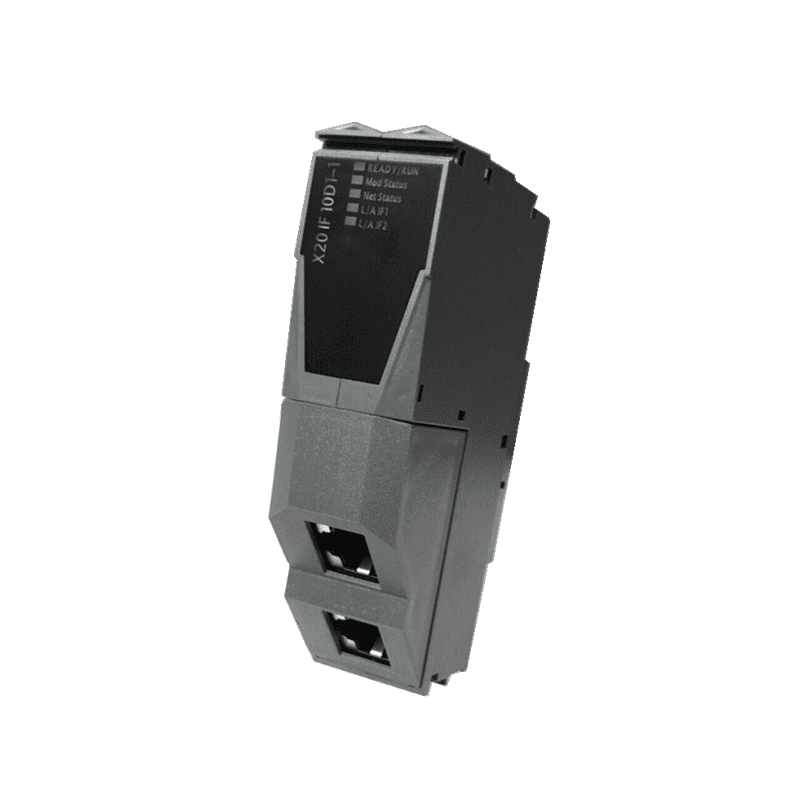
PLC System, I/O Sysytem, X20 System, X67 System, etc.
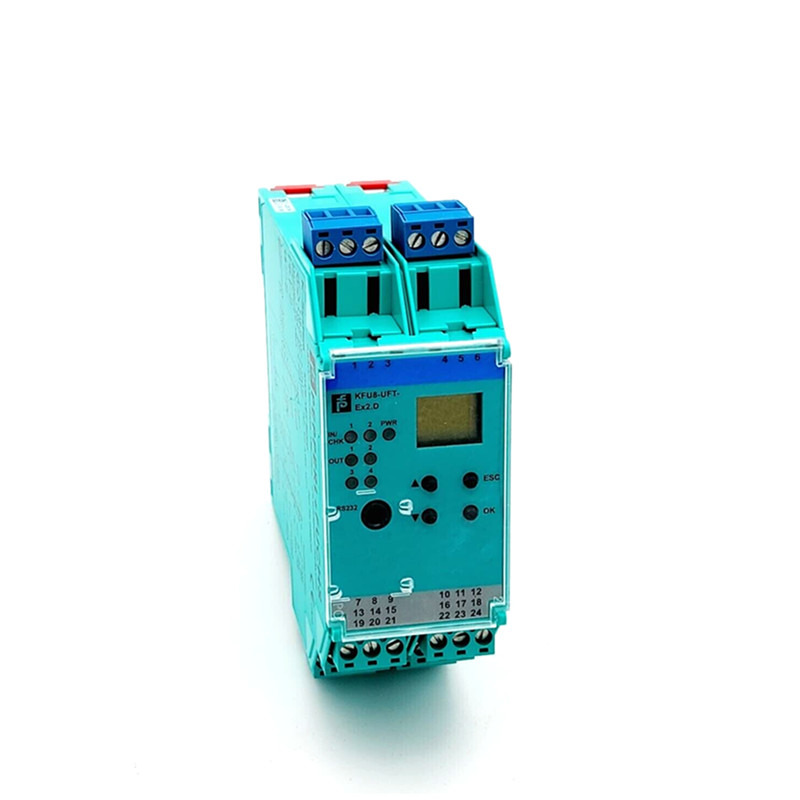
Isolated Barriers (K-System), etc.
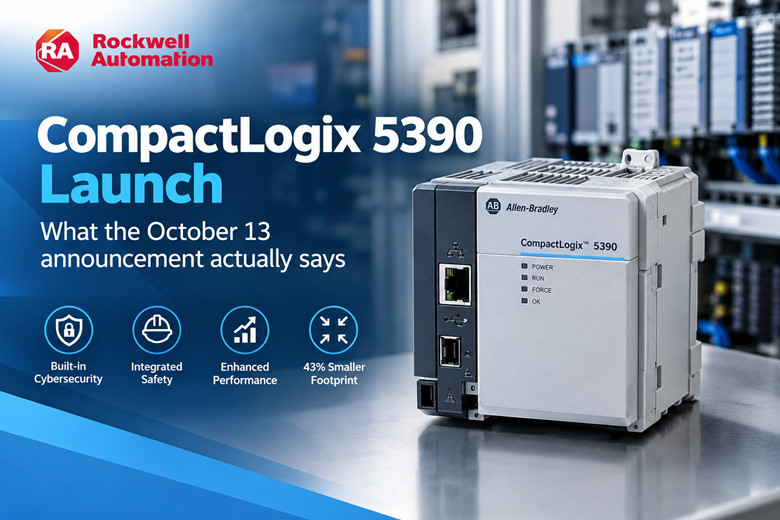
Rockwell Automation announced the CompactLogix 5390 controller in a press release dated October 13, 2026, issued from Milwaukee through PR Newswire. The document introduces the CompactLogix 5390 as the latest advancement in the company's Integrated Architecture controller family and states its purpose in one line: help machine builders and manufacturers optimize performance, security, safety, data and flexibility. It also makes one number public. The new controller has a footprint 43 percent smaller than previous CompactLogix 5380 controllers. That is the whole of the quantitative disclosure. Everything else in the release is capability language, a list of products the controller works with, and a quote from a product manager. For a buyer with budget authority, the useful work starts where the release stops. This analysis separates three things: what Rockwell stated, what those statements imply for a panel layout or a purchase order, and what nobody has published yet. The gaps are not a criticism of the announcement. They are the normal condition of a launch release, and they define the questions a distributor should be able to answer before anyone signs. What Rockwell announced on October 13 The release describes the 5390 as bringing together built-in cybersecurity, integrated safety and enhanced performance in a single control platform. Read that sentence the way a panel builder reads a bill of materials. Three functions that historically arrived as separate boxes are now offered inside one controller envelope, at least according to the marketing. Security gets a standard attached to it. Rockwell says the controller's capabilities are aligned to IEC 62443-4-2 and describes the product as ready for the EU Cyber Resilience Act. I/O gets a family name: support for local PointMax I/O, which the release says enables more modular architectures. The physical claim is the one that will end up in a quotation spreadsheet. Rockwell states the 5390 is 43 percent smaller than previous CompactLogix 5380 controllers and connects that reduction to two commercial outcomes, less panel space and more standardized designs across machine families. Compatibility is spelled out as a list rather than a diagram. The controller works inside the Rockwell Integrated Architecture ecosystem and integrates with PointMax I/O (5034), Kinetix motion, PowerFlex drives, Stratix networking, FactoryTalk Design Studio software and other visualization solutions. One quote carries the customer rationale. Siva Iyyamperumal, senior product manager at Rockwell Automation, said customers are being asked to do more than deliver performance and also have to address cybersecurity and safety requirements. The sentence is short and does a lot of framing work. It presents security and safety as buyer requirements that arrived from outside the machine, not as features Rockwell decided to add for their own sake. Table 1: What the October 13, 2026 Rockwell release states Item What the release says How to read the statement Product CompactLogix 5390 controller Named product, new launch Family Latest advancement in the Integrated Architecture controller family Positioning, no generation label Stated purpose Help machine builders and manufacturers optimize performance, security, safety, data and flexibility Positioning Core capability Built-in cybersecurity, integrated safety and enhanced performance in one platform Capability claim, no benchmarks Security standard Capabilities aligned to IEC 62443-4-2 Alignment, not a certificate number Regulation Described as ready for the EU Cyber Resilience Act Readiness claim, no declaration cited I/O Support for local PointMax I/O Capability claim, no module list Footprint 43 percent smaller than previous CompactLogix 5380 controllers The only numeric claim in the document Ecosystem PointMax I/O (5034), Kinetix motion, PowerFlex drives, Stratix networking, FactoryTalk Design Studio, visualization solutions Compatibility list without part numbers Commercial terms Not stated Absent from the release The date deserves a note of its own. October 13, 2026 is the manufacturer's own press release date, not a date assigned by a magazine, a distributor or a trade show. When this article refers to the announcement, it means the document Rockwell published that day and nothing later. The three claims that matter to a panel builder Most of the release is context. Three claims change decisions, and each one changes a different decision. The first is the footprint reduction. Panel space is the constraint that shows up last in a project and costs the most to fix. A controller that occupies 43 percent less footprint than the previous generation gives a designer room for terminal blocks, disconnects or a larger drive without changing the enclosure. Rockwell frames the benefit as standardization across machine families, which is the more valuable version of the claim. A single controller envelope that covers a range of machines means one panel layout, one set of drawings and one spare part held on a shelf. The second is security carried inside the controller rather than added beside it. For years, a machine that needed network security bought it as a separate appliance, an industrial firewall or a managed switch with filtering. Each of those devices needs its own panel space, its own power, its own firmware process and its own place in a support contract. A controller with security built in changes the architecture discussion, even if the release does not say what the built-in functions actually do. The third is the combination of safety and standard control on one platform. A machine with safety functions has usually needed either a dedicated safety controller or a safety-rated variant, and the split shows up in programming, wiring and validation. Rockwell's claim that integrated safety sits in the same platform as the control logic points toward a single project and a single tag database. It does not, on its own, tell an integrator what safety integrity level the product reaches. That figure is absent. Table 2: Claims in the release against evidence published so far Claim Release wording Verifiable today Still missing Smaller footprint 43 percent smaller than previous CompactLogix 5380 controllers The percentage itself, as a manufacturer claim Dimensions, mounting depth, weight Built-in cybersecurity Capabilities aligned to IEC 62443-4-2 The standard named, the alignment stated Certificate, assessed scope, security functions list CRA readiness Described as ready for the EU Cyber Resilience Act The claim exists in writing Declaration of conformity, timeline, covered products Integrated safety Integrated safety in a single control platform The phrase in the release Safety ratings, SIL or PL level, certified function set Enhanced performance Enhanced performance, no metric Nothing numeric Scan times, memory, task capacity, axis count Modular architecture Local PointMax I/O support The I/O family named Module list, channel counts, density, pricing Ecosystem fit Named integration with motion, drives, network, software The product families named Firmware version matrix, software release requirements Read the two columns together and the shape of the announcement becomes clear. Rockwell published the direction of travel with enough specificity to be quoted, and held back every figure an engineer would use to size a system. That is a deliberate sequencing choice, and it is common at launch. It also means the trade press, this article included, cannot yet write the sentence that buyers want most: what the thing costs and when it ships. Forty-three percent smaller: what it changes in a cabinet A footprint figure is an area figure. It describes the panel face the controller occupies, not the volume behind it, and the difference matters when a designer starts moving parts around. Consider how a typical compact control panel is organized. Wire duct runs horizontally across the back plate and eats usable area before any device is mounted. DIN rail sits between duct runs. Terminal blocks, breakers, relays and a power supply take the lower third. The controller occupies a slot near the top, and the space around it is reserved for cable bend radius and for the clearance a technician needs to land a screwdriver on a terminal. Reducing the controller's face area by 43 percent does not return 43 percent of the panel to the designer, because the clearance zones do not shrink at the same rate. What it does return is rail length and layout freedom. A narrower controller lets a designer keep a single horizontal rail for the control group instead of breaking the rail and adding a second tier. On a machine where the panel is already at its size limit, that can be the difference between keeping the enclosure and moving up a size, which changes the cutout in the machine frame, the door hardware, the cooling calculation and the shipping weight. Depth is the other half of the story, and the release says nothing about it. A controller that is smaller on the face but deeper behind the plate can collide with duct or with the back of a door-mounted HMI. Until dimension drawings appear, treat the percentage as a face-area claim and verify depth before committing a layout. Standardization is the commercial argument, and it is stronger than the space argument. A machine builder who runs four models on one panel architecture spends real money maintaining four sets of drawings, four spare-part lists and four sets of assembly instructions. If one controller covers the range, the bill of materials collapses toward a common core. The 43 percent figure makes that consolidation easier to justify internally, because the smaller envelope fits the smallest machine in the family without forcing a redesign of the largest. Field note: Do not resize an enclosure on the strength of a press release percentage. Panel thermal performance is driven by total watts dissipated inside the enclosure, not by the footprint of one component. A smaller controller with the same power loss puts the same heat into a smaller box, and the enclosure temperature rise can get worse. Confirm the watt figure and rerun the thermal calculation before you change the enclosure size or the filter arrangement. The claim that will decide most projects is not in the release at all. Buyers will want to know whether the 5390 fits an existing panel cutout pattern, whether the terminal arrangement is compatible with wiring already documented, and whether a machine built last year can take the new controller without redrawing the layout. None of those answers are published. PointMax I/O and the architecture around the controller Local PointMax I/O support is the least glamorous line in the release and possibly the most consequential for machine design. Local I/O means the slices sit on the controller's own backplane or rail rather than across a network, and that changes where the cabinet boundary falls. A distributed layout puts a network node in each zone of the machine. That is the right answer for a long line with stations spread over twenty meters, because it shortens home-run cable and lets a station be tested on its own. It is the wrong answer for a compact machine with a single enclosure, where every remote node adds a power supply, a network drop and a device that can fail. Local PointMax I/O points the design back toward the compact case. Slices stack next to the controller, wiring lands on the same rail, and the whole control group stays inside one enclosure. Rockwell's phrase for this is more modular architectures, which reads as an invitation to build a machine from a small set of repeated I/O blocks rather than a fixed channel count. The ecosystem list in the release is worth mapping before a project kickoff, because it describes the four interfaces a compact machine actually uses. Control layer CompactLogix 5390 controller (announced 2026-10-13) Local I/O PointMax I/O, 5034 family Motion Kinetix Drives PowerFlex Network Stratix Engineering FactoryTalk Design Studio Visualization Rockwell and third-party HMI options Not published Catalog numbers, memory, axis count, scan time, price A scope sequence that keeps a project honest, in the order the decisions actually get made: Fix the machine's I/O count and the number of motion axes on paper, before any part is selected. Decide which I/O must be local to the controller and which can sit on a remote drop, based on cable runs and test access. Confirm the drive and motion families the machine already uses, and check that the controller supports them in the software release you own. Confirm the network topology, including whether the machine needs managed switching for segmentation rather than an unmanaged block. Confirm the engineering software version required, and price the license and training impact if it is newer than what the shop runs. Only then ask for a quotation, with the I/O count and axis count attached so the distributor quotes a configured system rather than a headline part. Step three is where most compact machine projects lose time. A controller announcement describes a family, and a family supports a range of drives, but the specific pairing is governed by firmware and software versions that the release does not list. Rule of thumb: If a new controller requires a software version your maintenance team has not installed, budget the training and the first-project learning curve as part of the controller cost. On a single-machine order, engineering time usually exceeds the hardware delta. Cybersecurity wording: IEC 62443-4-2 and CRA readiness Two phrases in the release will be quoted more than any other, and both need parsing. IEC 62443-4-2 is the part of the IEC 62443 series that sets technical security requirements for industrial automation and control system components. It is written for the product, not for the plant. A vendor that meets it has documented and implemented a set of component-level requirements covering things like account management, integrity protection, confidentiality and event logging. Rockwell's wording is that the controller's capabilities are aligned to that standard. Aligned is not certified. A certificate naming the product and the assessed scope is a different document from a release sentence, and only the certificate tells a buyer which requirements were assessed and which were excluded. The EU Cyber Resilience Act is a horizontal regulation covering products with digital elements sold in the EU, and its main obligations phase in from December 2027. Readiness for that regulation is a forward-looking position, not a compliance finding. No product can hold a CRA declaration of conformity before the regime's obligations apply, which is why manufacturers are using the word ready rather than compliant. For a machine builder shipping into Europe, the practical question is not whether the controller is aligned. It is what evidence the builder can put in a technical file, and what obligations fall on the machine builder rather than the component supplier. Those obligations are split, and the split is exactly what a distributor should be able to explain. Warning: Treat aligned, ready and certified as three different words with three different meanings. If a quotation, a proposal or a customer specification requires a certified component, ask for the certificate and check that the product name and the assessed scope on it match what you are buying. A press release sentence is not a substitute, and a compliance officer will not accept one. The security claim also has a design consequence that the release does not spell out. Built-in security only helps if the machine's network architecture uses it. A controller with hardened functions behind an unmanaged switch on a flat network has the same exposure as before. Segmentation, account control and update policy are still engineering work, and they still belong in the project scope. What Rockwell did not publish This section exists because the absence of information is itself information, and because a buyer who assumes the missing details will be available at quotation time usually loses a week. The release contains no order or catalog numbers. It names product families, not purchasable items. A distributor cannot quote from the announcement, and a maintenance planner cannot add the controller to a spares list using the announcement. The release contains no memory figures, no axis counts, no scan times and no performance benchmarks of any kind. Enhanced performance is stated without a metric, a comparison or a test condition. Any article that prints a scan time for this controller at this point is guessing. The release contains no price. It contains no ship date and no availability window. It says nothing about distributor stock, first-allocation quantities or regional launch sequence. Buyers in the Middle East and Europe have no published indication of when the product reaches their channel. The release contains no end-of-sale date for the CompactLogix 5380. It does not describe the 5390 as a replacement, and it does not put a date on any transition. Anyone who tells you the 5380 stops being orderable on a particular date is repeating something Rockwell has not said. The release also omits the safety detail that a validation engineer needs: no safety integrity level, no performance level, no certified function list, no statement about which safety I/O families pair with the controller. None of this is unusual. A launch release is a positioning document written for a trade audience, and Rockwell published the parts that generate coverage. The technical publication, the firmware release notes and the price book come later, on their own schedule. Questions to ask a distributor before committing budget The release gives a distributor very little to work with, which makes the quality of the answers a useful test of the channel. Bring the I/O count and the axis count with you and ask the following. Table 3: Buyer questions for a distributor, and why each one matters Question Why it matters A useful answer looks like What is the order number for the configuration I need? The release has no catalog numbers, so the item cannot be quoted from the announcement A specific number from a current price book or configurator What is the ship date or availability window? No date was published, and a project schedule cannot absorb an open one A dated allocation or a written statement that none exists yet What is the price, including required software? Controller price alone understates the project if a software upgrade is needed Line-item pricing with license and support separated Which software version is required, and do I need to upgrade? Unpublished, and it drives training and validation cost A version number and a migration note What safety ratings apply, and which safety I/O pairs with it? The release states integrated safety without a rating Certified ratings and a compatible I/O list Is there a certificate for IEC 62443-4-2, and what scope does it cover? Aligned is not certified A certificate reference and the assessed product scope What is the firmware update and security advisory process? CRA readiness is a lifecycle position, not a one-time feature A published advisory channel and update policy What is the status of the 5380, in writing? No end-of-sale date was announced, and planning needs certainty A written statement of current lifecycle status Can I get dimensions and a thermal figure now? The 43 percent claim is a face-area figure A dimension drawing and a watt figure A checklist to take into the meeting: ☐ I/O count and axis count written down before the call ☐ Existing engineering software version confirmed ☐ Existing drive and motion families listed ☐ Enclosure dimensions and current thermal margin on hand ☐ Written confirmation of availability, price and software requirement ☐ Lifecycle status of the 5380 requested in writing, not verbally ☐ Safety rating and I/O pairing confirmed against a published document If a distributor cannot answer the first three items, the conversation is about a future product rather than a purchase. That is a legitimate conversation, but it belongs in a design review, not in a purchase order. Where the 5390 sits next to the 5380 in a live project Background first, because it explains why the comparison keeps coming up. The CompactLogix 5380, in the 5069 family, is the compact controller line that many panel builders specify today for machines in the mid range. Rockwell's Integrated Architecture includes Studio 5000 as the engineering environment that programs across the family. Neither of those statements is a specification, and this article does not offer one for either product. The 5390 arrives beside that installed base, not on top of it. The release says nothing about a replacement, a migration path or a date, and the 5380 remains the line that existing drawings, spare-part lists and maintenance procedures reference. For a new machine design, the 5390 is worth evaluating on the footprint and security claims alone, provided the missing figures arrive before the layout is frozen. For an existing machine that is already validated and shipping, changing the controller is a project with a validation cost that a smaller footprint rarely repays. For a builder running several machine models on one panel architecture, the standardization argument is the one that can justify the engineering hours. Spares strategy needs its own decision. A shop that holds one controller per machine family is exposed if a new family enters the mix before the old one leaves. Holding both is a cost, and the cost is smaller when the two share I/O and software, which is a question for the compatibility matrix rather than the release. Engineering labor is the line item buyers underestimate. A new controller in a plant means a software version decision, a programming standards review, a validation pass on safety functions and a training session for the people who will troubleshoot it at two in the morning. None of those costs appear on a quotation, and all of them land on the project. Bottom line: The CompactLogix 5390 is a credible direction with a thin public record. The footprint claim is specific enough to plan around once dimensions arrive. The security and safety claims are specific enough to start a compliance conversation, not to close one. No price, no ship date and no 5380 transition date have been published, so any budget built this month rests on assumptions that should be written down and dated. Dated timeline: what is confirmed and what is not A news analysis is only as useful as its separation of confirmed fact from expectation. The public record after the announcement is short enough to set out in full. 2026-10-13 CONFIRMED Press release issued from Milwaukee via PR Newswire 2026-10-13 CONFIRMED Product named: CompactLogix 5390 controller 2026-10-13 CONFIRMED Claim: 43 percent smaller footprint than the 5380 2026-10-13 CONFIRMED Claim: IEC 62443-4-2 alignment, CRA readiness wording 2026-10-13 CONFIRMED Claim: local PointMax I/O support Not stated UNKNOWN Order and catalog numbers Not stated UNKNOWN Memory, axis count, scan time, task performance Not stated UNKNOWN Price, currency and regional pricing Not stated UNKNOWN Ship date or availability window Not stated UNKNOWN Distributor stock and first allocation Not stated UNKNOWN End-of-sale or transition date for the 5380 The confirmed column is short, and it is still enough to act on. Designers can start a layout study. Compliance teams can open a question about certificates. Procurement can ask for a written availability position. Maintenance planners can note that a new family exists and resist the urge to standardize on it before the price book confirms it is orderable. The unknown column is where the risk sits, and it is not a small risk. A machine project that assumes an availability window and a price will either slip or absorb a change order. A panel layout that assumes a depth will be redrawn. A compliance file that cites a press release will be rejected. What the announcement does establish is direction. Rockwell is putting security and safety into the compact controller rather than selling them as adjacent products, and it is using panel space as the commercial argument for consolidation. Both moves point toward fewer boxes in a cabinet and a shorter bill of materials. Whether that direction reaches a given machine this year depends on documents Rockwell has not published. Until they appear, the correct posture is interest with a written list of open questions, and a quotation that names exactly which assumptions it rests on.
 October 28,2026

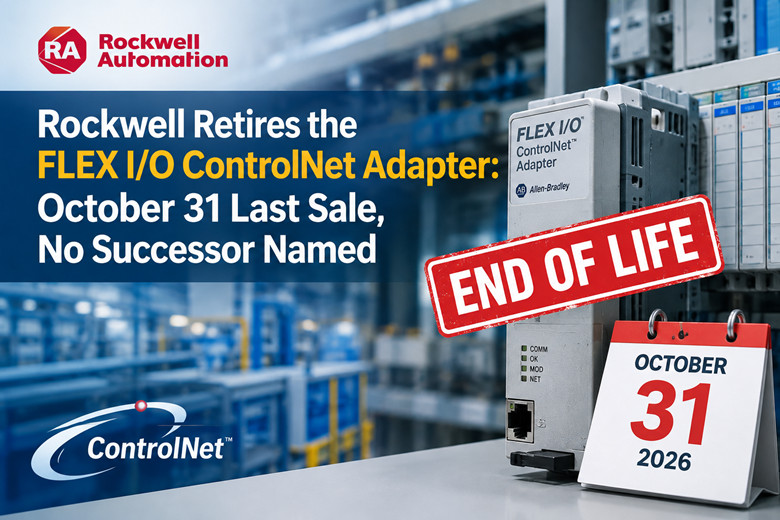
*Industry news | October 12, 2026* Rockwell Automation has set October 31, 2026 as the discontinuation date for the FLEX I/O ControlNet adapter, and there is no successor product named. The affected part numbers are 1794-ACN15, the standard ControlNet adapter, and 1794-ACNR15, the redundant-media version. That gives a plant roughly three weeks from today to place a last-time buy. After that, the adapter comes off the shelf in Rockwell's catalog, and the only route to a replacement is whatever distributors and independent suppliers still hold in stock. A stopped line does not care how clever the migration plan is. It cares that the adapter on the shelf fits. So the October 31 date is not an engineering footnote, it is a purchase order deadline, and it arrives in three weeks. Read the rest of the picture before you decide how much stock to buy. The ControlNet adapter is one part in a wider FLEX I/O retirement cycle, and the lead times on what remains tell you how much slack you actually have. The date that matters is October 31 October 31 is the last day the 1794-ACN15 and 1794-ACNR15 can be ordered from Rockwell. The product page carries lifecycle status End of Life with that discontinuation date, and the wording is direct enough to leave no room for interpretation: "Rockwell Automation announces that as of October 31, 2026, the Flex ControlNet Adapter will be discontinued and no longer available for sale. Customers are encouraged to remove references to the affected product(s)." That last sentence is the one worth reading twice. Rockwell is telling you to scrub the part number from your drawings, your bills of material and your maintenance procedures. It is not telling you what to put in its place. The replacement category on the product page is "Engineering Replacement." That is a specific and unhelpful phrase for anyone who owns this hardware. A functional replacement drops in and does the same job. An engineering replacement means the job can still be done, but the design changes, and the people who do the design work are not the ones holding the maintenance budget. No successor part number is listed. That is the detail that should drive your purchasing decision this month. When a vendor names a replacement, you can plan around it. You read the data sheet, you check the dimensions, you order one for the bench and you find out what breaks. When the replacement field is blank, you are the one writing the migration plan, and you are doing it without a vendor telling you which way to go. For a plant that keeps legacy ControlNet running because it works and because the capital was approved in a different decade, this is the moment where the platform question lands on the desk. Either you buy shelf stock to extend the life of what you have, or you accept that the ControlNet footprint is now on a countdown that you have not defined. The countdown is real either way. Rockwell has stopped selling. Every adapter in the field is now one failure away from being a problem you cannot buy your way out of at the usual channel. What is going out of production, and what is not The retirement does not touch every FLEX I/O adapter at once, and the gaps between the dates matter more than the dates themselves. Here is the model list, with what each one means for the shelf. 1794-ACN15, the FLEX I/O ControlNet adapter, non-redundant media. Lifecycle status: End of Life. Discontinued October 31, 2026. Replacement category: Engineering Replacement. No successor named. 1794-ACNR15, the FLEX I/O ControlNet adapter with redundant media. Lifecycle status: End of Life. Discontinued October 31, 2026. Replacement category: Engineering Replacement. No successor named. 1794-ACNR15XT, the Flex XT ControlNet adapter for extended temperature environments. Lifecycle status: End of Life. Discontinued December 31, 2027. Replacement product named: 5094-AENTRXT. 1794-AENT, the FLEX EtherNet/IP adapter with 10BaseT. Lifecycle status: End of Life. Discontinued September 30, 2028. Replacement category: Functional Replacement. Replacement product named: 1794-AENTR. 1794-AENTR, the FLEX I/O dual port EtherNet/IP adapter. Lifecycle status: Active Mature, which means it is still current. Rockwell lists an estimated lead time of 5 days. The two ControlNet adapters go first, and they go together. The XT variant, the one built for hot, cold and dirty conditions, gets an extra fourteen months and a named destination. The EtherNet/IP adapter gets almost two more years and a clean functional replacement. That pattern is not random. The platform is not being killed in one stroke. It is being retired from one network protocol at a time, and ControlNet is at the front of the queue. If you keep both a standard ControlNet adapter and an XT unit in the same plant, which is common on sites with a mix of climate-controlled panels and outdoor or washdown enclosures, the two are not on the same clock. Do not let one date blur into the other during a budget conversation. The XT users have a named successor and more time. The standard ControlNet users have neither. The EtherNet/IP side is the part of the answer that is still comfortable. The 1794-AENTR is Active Mature and Rockwell posts a 5 day lead time. That is not a part that is about to strand you. It is a part you can order through normal channels and get in the same week. The reason that matters here is that the EtherNet/IP adapter is the natural landing spot if the plant moves off ControlNet. It exists, it ships fast and it is not on a discontinuation list. That combination gives you an option, and the option costs less sleep than the blank field next to the ControlNet part. Start with what a FLEX I/O adapter actually does. One adapter connects up to eight FLEX I/O modules to the network. On the ControlNet side, that traffic runs on ControlNet V1.5. The adapter is the single point where a rack of I/O either talks to the controller or goes dark. One adapter, up to eight modules, one network connection. When that adapter fails, you do not lose one input point. You lose the whole rack. That is the number to hold onto when you are deciding how many to buy. The exposure per adapter is not the cost of the adapter. It is everything wired through it. Why a 73-day lead time makes this worse than it looks The 1794-ACN15 product page lists an estimated lead time of 73 days. Seven hundred and thirty hours of waiting, and that is Rockwell's own estimate on a part that is being discontinued in three weeks. Sit with that for a moment. The last date to order is roughly three weeks away. The lead time to receive is roughly ten and a half weeks. Those two numbers do not line up, and that mismatch is the whole story. An order placed on the last day of October does not arrive in October. It arrives somewhere in the first half of January, if the estimate holds. That is the trap in a last-time buy. People hear "last order date" and picture a firm deadline they can work backward from. In practice, a last-time buy is a commitment to wait, and you place it before you know what the next twelve months of failures will look like. For a maintenance planner, this changes the shape of the decision. You are not choosing between buying now and buying later at the same price and the same availability. You are choosing between securing stock at a known lead time and gambling that nothing in the rack fails while the channel is closing behind you. A 73 day lead time is also a signal about the supply chain behind the part. Long lead times on end-of-life hardware usually mean the part is built to order, or drawn from shrinking inventory, or subject to allocation. None of those conditions improve after the discontinuation date. They get worse, then they get scarce, then the only stock left is what is already sitting on shelves. The EtherNet/IP adapter's 5 day lead time sits right next to that 73 day figure on the same catalog, and the contrast is the point. One is a part you can order this afternoon. The other is a part you commit to months in advance to receive it at all. The practical reading is straightforward. Availability after October 31 is not a question of price. It is a question of whether anyone still holds the part. Distributor stock and independent suppliers are the channel, and that channel thins every month. If you have a critical rack, the lead time is the argument for acting this month rather than in the first week of November. The difference between ordering on October 24 and ordering on November 3 is not three percent of a purchase order. It is the difference between Rockwell's supply chain and whatever is left in the secondary market. If you need help locating what is still available, discontinued Allen-Bradley parts is a reasonable place to start a search, and it is worth doing it before the last sale date passes rather than after. The two realistic paths: keep the platform, or move to EtherNet/IP Once the adapter is gone from the catalog, the plant has two honest options. Everything else is a variation on one of them. The first path is to keep the platform. You buy enough adapters to carry the ControlNet racks through the horizon you are willing to plan for, you store them properly, and you keep running. This path does not require a capital project, a controller change or a shutdown window. It requires a purchase order and a shelf. The cost of this path is the shelf itself. Adapters that sit for years draw no power and cost nothing to hold, but they tie up working capital, they have to be stored somewhere dry and stable, and someone has to keep track of them. The benefit is that a failure on a Tuesday afternoon becomes a fifteen minute swap instead of a production event. The second path is to move to EtherNet/IP. This is where the plant stops treating ControlNet as a permanent fixture and starts treating it as a project. The 1794-AENTR exists, it is Active Mature, it ships in about 5 days, and it is the adapter the FLEX I/O platform is heading toward. Moving means more than changing the adapter. The controller side has to speak the same protocol, the network layout changes, the addressing changes, and the people who maintain the system have to learn a different set of tools. That is why this path is a project and not a purchase order. It is worth being clear about the size of the gap. ControlNet V1.5 and EtherNet/IP are different networks with different cable plants, different topology rules and different diagnostics. A rack does not migrate by swapping one card. The rack has to be rehosted on a network that the rest of the control system may or may not already speak. For some plants, that work is already underway. Any site that has been modernizing its control layer for the past decade probably has an EtherNet/IP backbone somewhere, and the FLEX racks are the last ControlNet island still connected. For those sites, the discontinuation is a schedule nudge, not a crisis. For other plants, the FLEX I/O ControlNet racks are the backbone. They were installed as the smart, flexible option at the time, and the rest of the plant grew up around them. For those sites, the second path is a genuine capital conversation, and the first path is the one that keeps the lights on while that conversation happens. The practical answer for most operations is a blend. Buy shelf stock for the adapters that carry the racks you cannot afford to stop, and start the engineering work on moving the racks that are either less critical or already near a planned outage. The one thing the blend is not, is free. Every month you spend deciding is a month the last-time-buy window is shorter, and the price and availability of whatever is left in the secondhand channel is a moving target. If you are weighing both paths, Rockwell Automation spares is a useful reference point for what is still being sourced and supplied in the aftermarket, so you can price the stock side of the decision against the project side. What an unplanned adapter failure actually costs the operation This is where people want a number, and this is where a responsible article refuses to give one. Downtime cost depends entirely on the plant, and any single figure quoted here would be invented, wrong for your site and useless as a budgeting input. Here is how to build your own number instead. Start with your line rate or your product throughput, whatever unit you already track output in. Multiply by the value of that output. That gives you the cost of an idle hour. Now add the labor that stands around while the line is down. Add the restart cost, which for some processes is real scrap and for others is hours of warm-up and re-qualification. Add overtime if you recover the lost volume with extra shifts. The result is your cost per stopped hour. That is the number that belongs in the decision, and it is a number only you can calculate. Then do the arithmetic that matters. If the adapter is on the shelf, the failure costs you a swap: call the electrician, power down the rack, change the card, power up, verify. A couple of hours on the wide end, often less. If the adapter is not on the shelf, the clock keeps running. You call your suppliers, you find out nobody has immediate stock, you wait. Now add the freight cost of an expedited shipment, and the premium that any scarce part commands when the seller knows you need it today. That gap between a swap and a wait is the entire justification for holding spares. It is also the number that makes a shelf of adapters look cheap. The 73 day lead time on the 1794-ACN15 turns a normal supply order into a production event. A part that is normally a next-week purchase becomes, after October 31, a part that might not be purchasable at all at the price or speed you are used to. There is a second cost that is easy to forget. A rack that has lost its adapter takes its up to eight I/O modules offline with it. If those modules feed a safety interlock, a batch recipe or a quality measurement, a "two hour electrical fix" can turn into a batch rejection or a quality hold that outlasts the repair by a wide margin. That is why the spares question is never really about the adapter. It is about the rack, and the rack is about whatever the plant does with the signals. If you have never built a downtime cost figure for your own site, do it now, while the part is still purchasable. It is much easier to justify a stock purchase with a real number on a spreadsheet than with a feeling that spare parts are probably a good idea. For plants keeping older platforms alive, legacy PLC hardware is often the practical source for the parts the original vendor no longer sells, and knowing your source before a failure is part of the same calculation. A spares audit you can run this week This is a walk-the-floor exercise and it does not need a project code. The goal is a single honest number: how many 1794-ACN15 and 1794-ACNR15 adapters your site actually depends on. Start at the panel. List every FLEX I/O rack that has a ControlNet adapter. For each one, write down the panel name, the process it serves, and whether the process is critical or can wait. Do not skip the awkward ones in remote corners of the plant; those are the racks most likely to be forgotten during planning and most painful to reach during a failure. Now count the adapters. Note whether each one is a 1794-ACN15 or a 1794-ACNR15. If your site uses redundant media anywhere, the ACNR15 count is the one to watch, because both versions share the same October 31 discontinuation and neither has a named successor. Next, check your own storeroom before you check anyone else's. Some sites are sitting on adapters they bought years ago and never recorded. A shelf count is free information, and it can change your whole buying plan in an afternoon. Then compare what you need against what you hold. The gap between those two numbers is what you are buying this month. As you go, note the failures. If an adapter has failed in the last couple of years, write down why. An adapter does not fail in isolation. Heat, vibration, dirty power and loose backplane connections all take a toll, and a rack with a history of failures will keep failing after the catalog closes. Racks with clean histories are the better candidates for the longer migration timeline. Two more things go on the audit sheet. First, list the XT racks separately. The 1794-ACNR15XT runs to December 31, 2027 with a named replacement in the 5094-AENTRXT, so it is a different line item with a different urgency. Mixing it into the standard ControlNet count will either overstate or understate your exposure. Second, write down who owns the decision. Every last-time-buy that stalls does so because the maintenance department wants the stock, the finance department wants the justification, and nobody wrote down whose signature is on the purchase order. Fix that before the last week of October. Once the audit sheet is done, the buying decision is arithmetic, not opinion. You know how many racks you carry, how many adapters you hold, and how many months of coverage you want. Multiply the gap by the unit cost, present it against your own downtime cost figure, and the conversation with finance runs itself. Do the audit this week even if the answer is "we already have enough." The audit is cheap. Finding out you were short is expensive. If your audit turns up gaps you need filled fast, industrial automation spares is the kind of source to have on standby before the deadline, not after it. The rest of the FLEX I/O lifecycle picture Zoom out, because the ControlNet adapter is not the only date on the calendar, and a plant that only reacts to this one will be doing the same exercise again in a year. Here is the sequence, in the order it arrives. October 31, 2026: 1794-ACN15 and 1794-ACNR15, the FLEX I/O ControlNet adapters, discontinued. Engineering Replacement, no successor named. December 31, 2027: 1794-ACNR15XT, the Flex XT ControlNet adapter, discontinued. Replacement product 5094-AENTRXT named. September 30, 2028: 1794-AENT, the FLEX EtherNet/IP adapter with 10BaseT, discontinued. Functional Replacement, replacement product 1794-AENTR named. Still current: 1794-AENTR, the FLEX I/O dual port EtherNet/IP adapter, Active Mature, estimated lead time 5 days. No discontinuation date listed. Read that as one continuous retirement of the FLEX I/O adapter family, protocol by protocol. ControlNet first, in two waves, with the standard adapters leading and the XT variant following fourteen months later. Then the oldest EtherNet/IP adapter, the 10BaseT version, with a functional replacement already named and a target two years out. The destination is consistent. Every retired adapter points, directly or eventually, at the EtherNet/IP side of the platform. The 5094-AENTRXT is the named replacement for the XT ControlNet adapter. The 1794-AENTR is the named replacement for the 1794-AENT. The 1794-AENTR itself remains Active Mature, shipping in about 5 days, with no retirement date announced. The pattern tells you what the platform wants to be. FLEX I/O stays. ControlNet goes. EtherNet/IP is where the racks are expected to land. For a maintenance manager, that pattern is more useful than any single part number. It means the migration plan you write today, whether it finishes next year or in five years, has one obvious direction. It also means the 1794-AENTR is the part you should understand now, because it is the adapters' future, and it is the one part in this whole family that is still easy to buy. Be precise about what Rockwell has and has not announced, because imprecision here costs money. What is documented is the sales discontinuation and the dates above. Rockwell has not announced an end of repair, an end of support, or a cut-off for spare parts through its own service channels. Do not let anyone in your next planning meeting claim otherwise. What the discontinuation does mean is concrete enough. The part is no longer sold. Availability becomes a question of existing stock. And the farther you get from October 31, the thinner that stock gets and the more the secondary market sets the price. That is the whole reason to treat the date as a purchase order deadline. It is not the day the part dies. It is the day the part stops being an order and starts being a search. Three weeks is not much runway, but it is enough to run the audit, count the racks, and place the order while the part is still a part number in a catalog rather than an inquiry to a supplier. The plants that will come out of this cleanly are the ones that spend the next week on the floor with a clipboard, not the ones that will spend the first week of November on the phone. The calendar is set. The successor field is blank. The only variable left is how many you decide to put on the shelf.
October 13,2026
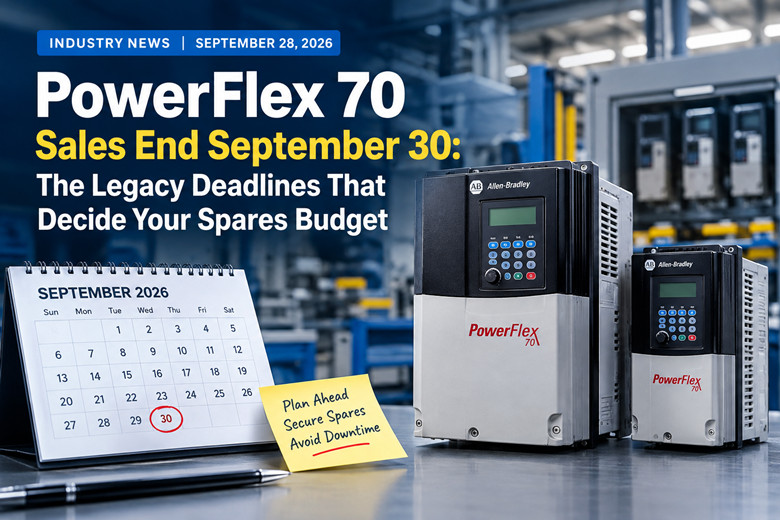
On Wednesday, Rockwell Automation stops selling new PowerFlex 70 drives. Not all of them, but the ones most plants actually have bolted into a cabinet. If you have a line running on a PowerFlex 70 and you have not yet decided what happens when the next one fails, that decision has now been forced on you. It is two days out. I have watched three of these transitions in fifteen years. The pattern does not change. The vendor announces, everyone nods, nobody budgets, and eighteen months later a maintenance tech is on a phone at 2 a.m. trying to find a rebuilt unit from a broker who will not answer the provenance question. That is the bill I am trying to keep you from paying. This is not a technical piece. You know what a drive does. This is about what the calendar costs, which parts you can still buy and when, and what you should put on a shelf before the dates arrive. What exactly ends on September 30, and what does not Read the announcement carefully, because the headline oversells it and the detail is where your budget lives. Rockwell's own PowerFlex 70 product page states: "Rockwell Automation announces the PowerFlex 70 AC Drive will be discontinued and no longer available for sale as of September 30, 2026. End of life status and discontinuation date only apply to the IP20/NEMA UL Type 1, IP54/NEMA UL Type 12, and Flange versions. The NEMA 4X versions remain in Active Mature status. To support your transition, we recommend modernizing to the PowerFlex 750 family of AC drives." That is the vendor's language, not mine. Two things matter in it. First, the NEMA 4X versions stay in Active Mature. If your washdown or outdoor installations run 4X enclosures, you keep a sales channel for now. Active Mature is not the same as Active, and it is not a promise of forever, but it is not a stop date either. Do not lump your 4X units in with the rest of the fleet when you build the audit. You will overspend on parts you can still order normally. Second, the stop applies to specific enclosure families, and Rockwell points users to its Product Lifecycle Status search tool to check individual catalog numbers. That is not a formality. A plant with forty PowerFlex 70 nameplates on a spreadsheet thinks it has forty problems. In practice the mix of frames, enclosures and option cards means you have maybe six or eight distinct catalog numbers that actually matter, and some of them are in a different lifecycle status than the rest. Pull the numbers. Read them one at a time. Do not trust the family name. The other half of this news cycle is Mitsubishi Electric, and there the deadlines are longer but the details are sharper. Two Sales and Service bulletins, both issued April 2026 and revised in August 2026, both citing difficulty obtaining components, cover the HF-KN series AC servo motors (Bulletin No. 26-07AE) and the MR-JN series AC servo amplifiers (Bulletin No. 26-06AE). The HF-KN has been on the market 17 years, since 2009. That is a long run for a servo motor, and it means the installed base across packaging, food processing and light assembly lines is deep. The bulletin sets a made-to-order transition on March 31, 2027, order acceptance through March 31, 2028, last shipment and production end on March 31, 2029, and repair acceptance and parts supply through March 31, 2036. A third bulletin, No. 26-09AE, covers the MR-EM340GF Simple Motion board and the SW1DND-EMSDK-B MELSOFT EM Software Development Kit. Same dates. More on that one shortly, because the replacement part is the awkward one. The calendar, in the order it will hit you Here is the sequence. No table, just the dates in the order they land, because that is how you build a purchase order schedule. · September 30, 2026: new PowerFlex 70 sales end for IP20/NEMA UL Type 1, IP54/NEMA UL Type 12, and Flange versions. Two days from now. If you need a new unit in one of those enclosures, this is the last full business week and it is already ending. · December 2026: the FX3G series PLC reaches its discontinuation date, following a June 2025 Mitsubishi announcement that set a last order date of June 2026 with the FX5UJ as the recommended successor. If you missed that order date, you are already in the secondary market for FX3G hardware. Note this one, because it is the case study for the whole article: the notice came eighteen months ahead, the last order date passed quietly in June, and the discontinuation date arrives in December with nobody's attention on it. · March 31, 2027: HF-KN servo motors, MR-JN servo amplifiers and the MR-EM340GF motion board and its SDK all move to made-to-order. This is the first real pinch point. Made-to-order means lead times stretch and the vendor is building to demand, not to stock. If you have a project commissioning late 2027, that date is on your critical path whether your project manager knows it or not. · April 2027: CE and UKCA marking removal takes effect on orders received on or after that date, for the same three Mitsubishi product groups. This is a different kind of deadline, and I will give it its own section below. · March 31, 2028: order acceptance closes on HF-KN, MR-JN and the MR-EM340GF. After this date you cannot place an order at all. This is the hard buy date. Everything before it is planning. After it, you are buying from someone else's shelf. · March 31, 2029: last shipment, and production ends, for HF-KN, MR-JN and the MR-EM340GF. Whatever was ordered by March 2028 ships by this date and then the factory stops. · March 31, 2036: repair acceptance and parts supply end for the same Mitsubishi product groups. Seven years of repair window after production ends. That is generous compared to what most drive lines get, and it is the single most important line in this article for anyone panicking about a 2029 date. Read that list once more and notice what is missing. Rockwell has published a sales end for the PowerFlex 70. Rockwell has not, on the material I can find, published an end of repair, end of support or spare parts cut-off for the same drive. I am not going to invent one for them, and you should be suspicious of any supplier who tells you a Rockwell repair window that the vendor has not stated. The absence of a date is not a runway. It is an absence of a date. Plan accordingly. Why April 2027 is not like the other dates Every other date on that calendar is about volume: can I order it, will it ship, can it be repaired. April 2027 is about paperwork, and paperwork is the deadline that catches European and UK plants off guard. Both the HF-KN and MR-JN bulletins state, in Mitsubishi Electric's own words: "The CE marking will be removed from the [series] because it does not comply with the EU Cyber Resilience Act (CRA). In conjunction with the removal of the CE marking, the UKCA marking will also be removed. The orders received by Mitsubishi Electric on or after April 2027 will be supplied without the CE marking and UKCA marking." I am reporting that as the vendor's statement. I am not going to argue the legal reading of it, because that is for your compliance people, not for a spares buyer at 6 a.m. on a Monday. What I will tell you is the practical consequence, and it is a procurement consequence, not a technical one. If your plant is in the EU or the UK and your machinery documentation references CE or UKCA marked components, an order placed in April 2027 arrives with a rating plate that looks different from the one in your existing drawings. That is a conversation with your quality manager, your notified body if you have one, and whatever customer audit sits over your head. It is not a conversation you want to have for the first time the week you need the part. The hazard gets worse, and the bulletins say so plainly: both the former and the new versions may be in distribution at the same time depending on stock status. That means a distributor with old marked stock and a distributor with new unmarked stock can both quote you the same catalog number on the same day, and the marking on the plate may differ. If you need a specific marking, you have to specify it on the purchase order and you have to confirm it at goods-in. Assume nothing from a part number alone. For a plant in the Middle East or the Americas, this matters less directly, though it matters if you export machinery into Europe or if your OEM builds to European documentation. And it matters for resale value on anything you later sell into the EU. Know which of your three audiences applies before you decide how much of the April 2027 date is your problem. The MR-EM340GF has one more wrinkle. Mitsubishi states that the recommended replacements, the motion control software SWM-G or the motion control board MR-EM441G, are not compatible with the MR-EM340GF and differ in specification. That is the vendor's language, and it is about as clear as a vendor gets. There is no drop-in. The replacement SDK is SW1DND-EMMSDK-B, and the bulletin references Mitsubishi document No. 26-21E, titled "Change in Packaging Labels and Rating Plates due to Enforcement of EU Cyber Resilience Act." If you run an MR-EM340GF, the part is not a stock buy. It is a migration project with its own engineering hours, and it belongs in the capital plan, not the consumables budget. What this costs, and what it does not Let me separate the fear from the bill, because the two are not the same number. The fear is that September 30 means your PowerFlex 70 fleet is orphaned and every failure is a line-down event. That is not what the announcement says. Sales end is not support end. Rockwell stops selling new units in three enclosure families. It has not announced a repair cut-off. Your existing drives keep running, and the installed base is large enough that the third-party repair and remanufacturing market will serve it for years. For legacy drive spares, the practical question is not whether parts exist. It is who has them and what condition they are in. The fear on the Mitsubishi side is the same, and the bill is smaller than you think. The repair window runs to March 31, 2036. That is seven years past production end. Most plants will have migrated off HF-KN and MR-JN long before that, because the replacement lines exist and are documented: HF-KN053(B) to HK-KT053W(B), HF-KN13(B) to HK-KT13W(B), HF-KN23(B) to HK-KT23W(B), HF-KN43(B) to HK-KT43W(B), HF-KN73(B) to HK-KT7M3W(B) on the motor side, and MR-JN-10A to MR-J5-10A, MR-JN-10A1 to MR-J5-10A, MR-JN-20A to MR-J5-20A, MR-JN-20A1 to MR-J5-20A, MR-JN-40A to MR-J5-40A on the amplifier side. If your architecture runs an MR-JN-10A1 or MR-JN-20A1 on a 1-phase 100 V AC input, note that Mitsubishi requires the MR-CM08K1 simple converter in combination. That is a line item people miss when they quote the swap. The Mitsubishi bulletins do add one honest caveat worth reading twice: repairs may not be possible once component inventory is exhausted. So the repair window is a maximum, not a guarantee. Anyone telling you 2036 is a certainty has not read past the date line. That leaves the real variable, and it is not the vendor. It is the secondary market. Once orders close, every part you buy comes off someone's shelf. Condition and provenance become the deciding factors, and those do not appear on a data sheet. A remanufactured MR-JN that has been tested on a load bank with a documented repair record is a different asset than a unit pulled from a decommissioned panel and wiped down. Both can be quoted at the same price. Only one belongs on a critical line. The way you control that is by knowing your supplier's testing procedure before the emergency, by keeping serial numbers on your own units so you can trace what came back from repair, and by deciding in advance which of your lines can tolerate a used unit and which cannot. For a plant, servo drive parts and drive spares bought from the secondary market are a legitimate, budget-saving route, provided the supplier tests, documents and warrants. The moment a supplier cannot describe their incoming inspection, the price stops being the point. The decisions this forces this quarter You have a short list and a long list. Do the short list in the next ninety days, before the March 2027 date starts pulling lead times. 1. Run a spares shelf audit against actual installed units. Walk the floor, pull every nameplate, and record catalog number, serial number, enclosure type and date of installation. This is the step everyone skips and it is the step that saves the most money. You will find drives on the shelf that belong to lines you decommissioned in 2019, and you will find lines running hardware that nobody has a spare for. 2. Build a clean catalog number list, one line per distinct number, with quantity installed and quantity on the shelf. On the PowerFlex 70 side, sort the list by enclosure family and check each number against Rockwell's Product Lifecycle Status tool rather than assuming the family status applies. On the Mitsubishi side, separate the three groups: HF-KN, MR-JN, MR-EM340GF. 3. Set a stock buy date tied to the real deadline, not the scary one. For Rockwell that date is now, for the IP20, IP54 and Flange units you still run. For Mitsubishi the hard date is March 31, 2028 for order acceptance, and the made-to-order transition on March 31, 2027 is the date by which lead times start hurting you. Anything you intend to buy new, buy before March 2027 or accept the lead time. 4. Start the migration case for the capital plan, not for the emergency. A migration case is a one-page document: how many units, what the replacement part number is, what changes in the panel, what the engineering hours look like, and what the plant loses if it does not do it. For MR-EM340GF that document is mandatory because the replacement is explicitly not compatible. For PowerFlex 70, Rockwell recommends the PowerFlex 750 family, so the case is a modernization, and modernizations go in next year's budget, not this month's emergency account. 5. Brief your quality or compliance contact on the April 2027 marking change, before it becomes a goods-in problem. It is a fifteen-minute conversation today and a stranded shipment later. That list is small on purpose. You are not going to migrate forty drives this quarter, and you should not try. You are going to know what you have, buy the parts that go away first, and put the rest on a documented track. Where a spare parts supplier fits I am not going to pretend a parts supplier solves a lifecycle problem. We do not. What a good supplier does is narrower and more useful: it holds stock on the numbers you are about to lose, it can tell you which units it has tested and how, and it does not disappear during the week you actually need the part. What you should ask any supplier quoting you on discontinued hardware, and ask before you need them: Do they test, and on what? A load test on a drive and a run test on a servo are minimums. Ask for the procedure. Can they trace provenance on a used or remanufactured unit? If they cannot describe where a part came from, treat the unit as unknown condition. Do they hold buffer stock on the numbers you care about, or do they source to order? Sourcing to order means your lead time equals their lead time, which is exactly the problem you were trying to solve. Will they confirm the marking on the rating plate for Mitsubishi parts after April 2027? If you need CE or UKCA, this is the question that separates a supplier who understands the change from one who has not read the bulletin. The honest answer for most plants is a mixed model. Critical lines get new or vendor-repaired units. Non-critical lines and low-frequency spares come from tested secondary stock. Automation spares sourced that way, with documented testing, beat an unplanned line-down every time. Get that mix decided before the calendar decides it for you. FAQ Does September 30, 2026 mean my PowerFlex 70 drives stop working or stop being supported? No. It means Rockwell stops selling new units in the IP20/NEMA UL Type 1, IP54/NEMA UL Type 12 and Flange families. Your installed drives keep running. Rockwell's published material documents the sales end and points users to its Product Lifecycle Status tool for individual catalog numbers. It does not publish a repair or support cut-off for this drive, and you should not accept a supplier's claim that it does. My plant runs NEMA 4X PowerFlex 70 units. Am I affected? Not by this date. Rockwell states the NEMA 4X versions remain in Active Mature status. Active Mature is not the same as Active, so keep it on your watch list, but you are not in the September 30 stop. What is the actual last date I can buy HF-KN motors and MR-JN amplifiers? Per the Mitsubishi bulletins, order acceptance runs through March 31, 2028, and last shipment and production end is March 31, 2029. The made-to-order transition happens earlier, on March 31, 2027, so treat March 2027 as the date lead times start working against you. Is the April 2027 CE marking change a reason to stop using these parts? That is a decision for your compliance function, not for the parts buyer. Mitsubishi Electric states that CE marking will be removed because the series does not comply with the EU Cyber Resilience Act, that UKCA marking will also be removed, and that orders received on or after April 2027 will be supplied without either marking. What it means for your machinery documentation depends on your market and your customer requirements. Can I buy the replacement part and drop it in? On the motor and amplifier side, the replacement lines are documented (HF-KN to HK-KT, MR-JN to MR-J5), and there are combination notes, including the MR-CM08K1 simple converter for certain 1-phase 100 V AC configurations. On the MR-EM340GF, Mitsubishi states plainly that the recommended replacements are not compatible and differ in specification. That one is an engineering project, not a part swap. How long should I plan on the repair route? Mitsubishi bulletins set repair acceptance and parts supply through March 31, 2036 for HF-KN, MR-JN and the MR-EM340GF, with the caution that repairs may not be possible once component inventory is exhausted. Plan the repair route as a bridge, not as a permanent strategy. The FX3G situation is already past its last order date. What does that tell me? It tells you the notices are accurate and the dates are real. Mitsubishi announced the FX3G discontinuation in June 2025, set a December 2026 discontinuation date and a June 2026 last order date, with the FX5UJ as successor. The last order date passed. If you were not watching, you are now buying FX3G hardware from stock. That is exactly the position you do not want to be in with HF-KN and MR-JN in 2028. Should I buy a lifetime supply of spares now? Rarely. Shelf stock costs money, ties up capital and can degrade. Buy what your failure history says you consume over the made-to-order window plus a buffer, not a lifetime. The exception is a part with no compatible replacement, like the MR-EM340GF, where the case for holding stock is stronger because the alternative is a redesign. SEO fields - do not paste this block into the website Meta Title PowerFlex 70 Sales End September 30: Legacy Deadlines Meta Description Rockwell PowerFlex 70 sales stop September 30, 2026, and Mitsubishi HF-KN and MR-JN run out in 2029. The deadlines, the CE marking change and what to stock now. URL Slug powerflex-70-sales-end-legacy-automation-deadlines-2026 Category news Publishing steps: 1) paste Meta Title + Meta Description into the Yoast SEO fields, 2) set the URL slug, 3) pick the category, 4) request indexing in Search Console. Site: tztechio.com
September 28,2026
Holiday Notice: Mid-Autumn Festival and National Day 2026 Dear customers, Our office and warehouse in Xiamen will be closed for two public holidays: Mid-Autumn Festival: September 25 to September 27, 2026 National Day: October 1 to October 7, 2026 We are back at work on Thursday, October 8, 2026. September 28 to 30 are normal working days. Orders. Orders confirmed and paid by September 30 will be dispatched before the National Day closure, subject to stock. Orders received during the closures are processed in the order they arrive, starting October 8. If you need parts in October, send your enquiry before September 30 so we can confirm stock and shipping in time. Support. Email and WhatsApp messages are still received during the holiday, but replies will be slower. For urgent breakdowns, send the part number and fault details to WhatsApp +86 175 5077 6091 and we will come back to you as soon as we reopen. Thank you for your continued business. We wish you a good week. Xiamen Zantang Technology Co., Ltd Tel / WhatsApp: +86 175 5077 6091 Email: info@tztechautomation.com tztechio.com
September 24,2026
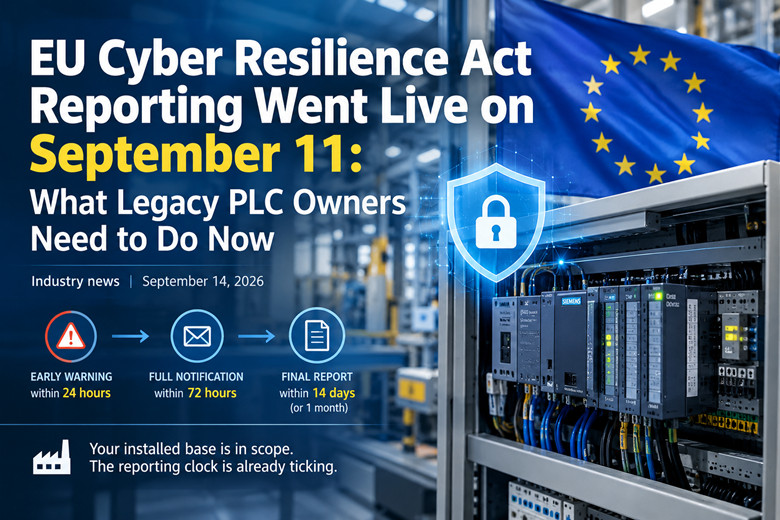
*Industry news | September 14, 2026* The date that matters to you is not 11 December 2027. It is 11 September 2026, three days ago. On that Friday, the reporting duties under the EU Cyber Resilience Act started to apply, and they apply to the equipment already bolted into your cabinets, not to the equipment you might buy next year. If a controller, HMI or drive on your floor has a data connection and someone actively exploits a vulnerability in it, the company that made it now has 24 hours to raise an early warning and 72 hours to file a full notification with an EU platform. Nobody sent you a letter about it. Your spare parts shelf and your capital plan were both built around the December 2027 date, because that is the date everyone quoted, and that date is still real for the CE marking side of things. It just is not the date that governs reporting. Those two dates now sit three months and roughly fifteen months apart, and the gap between them is where a plant gets caught out. Here is the operational version. Reporting started. Your installed base is inside it. Your patch path for most of that installed base probably does not exist. Those three sentences together are the whole story, and the rest of this piece is about what a maintenance or plant manager can actually do with them. What changed on September 11 The Cyber Resilience Act is Regulation (EU) 2024/2847. It entered into force on 10 December 2024. Article 71(2) is the article that sets out when the pieces switch on, and it does so in stages rather than all at once. Chapter IV, the part about notified bodies, has applied since 11 June 2026. Article 14, the reporting duty, applies from 11 September 2026. The main conformity regime, meaning the Annex I essential requirements, the technical documentation and the CE marking, applies from 11 December 2027. On the Friday just gone, what became live is the obligation on manufacturers to report. From 11 September 2026, a manufacturer must report actively exploited vulnerabilities and severe incidents affecting the security of products with digital elements. This is the Article 14 reporting duty. In plain terms: if a connected product the manufacturer sells is being exploited in the wild, the manufacturer has to tell the authorities, and it has to do it fast. Fast means measurable. Once the manufacturer becomes aware, it files an early warning within 24 hours, a full notification within 72 hours, and a final report no later than 14 days after a corrective measure is available for an actively exploited vulnerability, or within one month of the 72-hour notification for a severe incident. Reporting is done once, through the CRA Single Reporting Platform, or SRP, which was established by ENISA under Article 16 and was operational on 11 September 2026. The notification goes to the CSIRT of the manufacturer's main establishment and gets shared with ENISA and the other national CSIRTs. ENISA published the list of CSIRT coordinators covering all 27 member states on 4 September 2026, which tells you the plumbing was being finished right up to the deadline. There is one detail circulating that gets misread, and it matters because it separates a public-relations problem from a legal one. Commission Delegated Regulation (EU) 2026/881, adopted on 11 December 2025, lets a receiving CSIRT delay onward dissemination on cybersecurity grounds. Read that carefully. It restricts who sees a report. It does not change when it is filed. Nothing in that delegated regulation pauses the manufacturer's own filing clock. If you are talking to a vendor who suggests the clock might be paused, the clock is not paused. Then there is Article 14(8), which adds a separate duty to inform impacted users. If the manufacturer does not do that in time, the notified CSIRTs may inform users themselves where they judge it proportionate and necessary. That is the part to keep in your back pocket during a warranty conversation, because it is the regulation's own answer to the question of who eventually tells the plant. If the maker stays quiet too long, the regulator can go around them. Why legacy equipment is caught The assumption I hear most often, and I have heard it in almost those words from people who should know better, is that anything sold before December 2027 is grandfathered and therefore irrelevant to this regulation. That is half true, and the half that is false is the expensive half. Article 69(2) grandfathers products placed on the market before 11 December 2027 unless they undergo a substantial modification after that date. So an untouched machine, sitting there doing its job with the original firmware and no significant changes, is outside the CE marking and Annex I essential requirements. Fine. For an unmodified line you are not going to get dragged into a conformity project, and nobody is going to ask you to re-document a panel that was built in 2011. Article 69(3) overrides that specifically for reporting. The Article 14 duty applies to all in-scope products with digital elements placed on the market before 11 December 2027, with no age cutoff and no carve-out for old equipment. Sit with the phrase "no age cutoff" for a second. It does not say five years, it does not say ten years, and it does not say "still supported." It says all in-scope products placed on the market before that date. Now combine that with the scope rule. Products with digital elements whose intended or reasonably foreseeable use includes a direct or indirect logical or physical data connection to a device or network are in scope. Your plant runs Siemens, Rockwell, Mitsubishi and a long tail of other brands, mostly as controllers, HMIs, drives and I/O blocks. The ones that sit on Ethernet or on any fieldbus that reaches the plant network, or that anyone can plausibly connect a laptop to, tick that box. There are explicit exclusions, and they are narrow and specific: medical devices, vehicle type approval, civil aviation products, marine equipment, products developed exclusively for national security or defence, and identical spare parts. A packaging line controller is not on that list. So here is what that means for a plant running controllers and HMIs installed between 2005 and 2020. You are not the obligated party. The manufacturer is. But the equipment you own is the subject of the obligation, and it is subject to it without any age limit. A thin-client panel PC commissioned in 2008 is as much a candidate for a reported exploited vulnerability as a unit shipped last month, as far as the reporting duty is concerned. The item on your floor has not changed. What changed is that the company that made it now has a legal clock attached to what happens to it. There is a practical consequence buried in that, and it is the one I would want my own team to understand. In a reporting regime with a 24-hour clock, the manufacturer's willingness and ability to know what is happening in old equipment becomes a compliance asset. Vendors who cannot see into a decade-old build are not off the hook. They have to report what they know. But the flow of information runs through their support and security channels, and if your plant is not in that stream, you will be the last to know. The part that should worry a plant manager more than the reporting Reporting is somebody else's deadline. The patch question is yours, and it is worse. Think about the sequence. A vulnerability in an out-of-support controller gets actively exploited. The manufacturer becomes aware, and it starts a 24-hour clock and then a 72-hour clock. Under Article 14 it has to say what it knows. What it does not have to do is fix the thing. The Commission has been explicit that a manufacturer may genuinely be unable to investigate a vulnerability in a legacy product, because build environments cannot be recreated, dependencies are unavailable, or the people who knew the code have left. In that case the manufacturer must still notify, but is not required by the regulation to meet the other obligations, such as vulnerability handling. The duty is to report what is known, not to reopen a decade-old build. Read that as an operations manager and the sentence has teeth. An out-of-support controller will not get a patch. It may well get reported. So there is now a defined path where the world learns that your line is exploitable, the maker files the paperwork on time, and nothing physically changes at your plant. The report is a disclosure event, not a remedy. That reframes the support period from a nice-to-have procurement line into a security date, and it shifts where the risk sits. Under Article 13(8), a manufacturer must define a support period for vulnerability handling, at least five years or the expected in-use period if shorter, starting when the product is placed on the market, and must disclose the support period end date at the point of purchase in at least month and year format. Under Article 13(9), each security update must remain available for at least 10 years after issuance, or for the remainder of the support period, whichever is longer, and security updates must be supplied free of charge, with a narrow exception for tailor-made business products. A minimum support period of five years is a floor set by regulation, and it is short. Five years from a purchase order in 2026 lands in 2031. Five years from a 2019 order landed in 2024, which is already behind us. I have panels in this plant older than some of the people who now run them. So the stated support end date, in month and year, is now the closest thing you have to an expiry label on a control asset, and it belongs in the asset register next to the model number, not in a supplier's marketing deck. The migration argument follows from that without any engineering. If the support end date is the last date you can expect a vulnerability fix, and the reporting regime reaches back before 2027 with no age cutoff, then an end-of-support date is a security date. A dated security date is a procurement problem. It is not an IT problem, because IT does not buy the controller, does not stock the spare, and does not own the line when the migration window closes. It sits on the maintenance manager's desk, and eventually on the capital committee's desk. What the plant has to do None of this requires you to become a compliance officer. It requires four pieces of work that a manager can assign to named people, and one of them can start this week. Build an asset list of connected control equipment, with the support period end date next to each item. The word "connected" is doing real work there. Anything on the plant network, anything on a fieldbus that bridges to it, anything an integrator or a vendor laptop plausibly touches. If you have a CMMS or an asset register that already holds the tag numbers, extend it rather than starting a parallel spreadsheet, because a second list will rot. Ask suppliers and distributors for the declared support end date in writing. For anything bought from now on, treat that date as a specification alongside I/O count and price. Nobody negotiates a controller without knowing how many digital inputs it has. From this quarter, the support end date belongs in the same conversation, in months and years, in writing, on the quote if you can get it. A verbal answer is not a support statement. Put every automation vendor's security advisory channel on someone's job description. Not a shared inbox nobody reads, and not a personal email that leaves when the person does. A named role, with a backup, and a bench check that both people can log in. Vendor advisories are how you find out that a vulnerability has moved from theoretical to actively exploited, and that is the trigger point for everything in this article. Sort the equipment into what can still be patched and what cannot. That split is not a compliance exercise. It is your migration queue. Everything inside a support period goes on the maintain list. Everything outside it goes on the migration list, ordered by how much the line costs you when it stops. That is the whole triage. You do not need a risk model to draw that line; you need the support dates from step two and a view on criticality, which you already carry in your head. Fold 11 December 2027 into the capital plan rather than treating it as an IT matter. That is the date the full conformity regime applies, and it is also the deadline that has been quoted at you for two years, which is exactly why it is the wrong date to plan around alone. If your migration queue only gets funded when the 2027 date starts to bite, you will be executing migrations under time pressure with no negotiation room on lead times or price. Funding the queue a year early is cheaper than funding it in the last quarter of 2027, and the security argument is now the reason to do it rather than a slogan. There is one more thing that belongs in a manager's head, and it is about relationships rather than process. Your route to a support statement is usually the distributor or reseller who sold you the module, or the integrator who specified it. Those people have the manufacturer relationship you do not, and they can get a written answer where your general inquiry goes nowhere. This is a reason to keep a small number of parts and support relationships in decent condition rather than chasing the cheapest quote on every single transaction. When you need a support end date in writing, a documentation response or a last-time-buy allocation, you find out quickly who actually wants your business. Timetable Date | What applies 11 June 2026 | Chapter IV of the regulation, on notified bodies, applies. 11 September 2026 | Article 14 reporting duties apply. Manufacturers must report actively exploited vulnerabilities and severe incidents affecting the security of products with digital elements. Once a manufacturer becomes aware | The reporting clock runs: early warning within 24 hours, full notification within 72 hours, and a final report no later than 14 days after a corrective measure is available for an actively exploited vulnerability, or within one month of the 72-hour notification for a severe incident. 11 December 2027 | The full manufacturer conformity regime applies, including Annex I essential requirements, technical documentation and CE marking. Two notes on that table. First, the reporting row in the middle is not a one-off event. It is a standing obligation that fires each time a manufacturer becomes aware of an actively exploited vulnerability or a severe incident, which is why the clock, not the date, is the thing to keep in view. Second, the two dated rows are not the same project. The September 2026 row is about disclosure and it is already running. The December 2027 row is about conformity and it is what your capital plan has to absorb. Penalties, briefly Article 64 sets the money. For breaching the Annex I essential requirements or the Article 13 and Article 14 obligations, administrative fines run up to EUR 15 million or, for an undertaking, up to 2.5 percent of total worldwide annual turnover for the preceding financial year, whichever is higher. Other obligations carry up to EUR 10 million or 2 percent. Supplying incorrect, incomplete or misleading information to notified bodies or market surveillance authorities carries up to EUR 5 million or 1 percent. Member States set the rules on penalties, so the practical enforcement shape will vary by country. That is the manufacturer's exposure. It is not yours, and I would not invent a number for what it costs a plant, because it does not. What it does do is explain behavior. A supplier facing a potential EUR 15 million fine, or 2.5 percent of group turnover, has a hard reason to build a real vulnerability process: intake channels, triage, an ability to say something within 24 hours. It also has a hard reason to be careful about what it writes down. Expect documentation requests around supported life, update availability and known-issue status to get more serious over the next eighteen months, and expect a vague verbal answer to be replaced by a templated written one. That is a good outcome for a buyer, on balance, because a manufacturer that has to measure something tends to manage it. The buyer's job is to ask the question in a form that produces a dated answer rather than a brochure. I would not read too much else into the penalty numbers. Nobody is being fined today, and I am not aware of any enforcement wave arriving before the conformity regime starts in 2027. The reason to care now is that the September date is live and the incentive it creates reaches into how much information you get about your own plant. The spare parts angle Identical spare parts are excluded from the scope of the regulation. That exclusion is real and it is specific, and it is relevant to what a parts supplier sells. If you buy an identical replacement module to swap into a cabinet that already has that module, the spare part itself is not a product with digital elements under this regulation. Do not turn that into a compliance answer, because the controller those parts go into is not excluded. The exclusion carves out the spare part; it does not carve out the device the part sits in. A plant cannot retire its exposure by buying one more identical module for the shelf. When that controller becomes the subject of a report because a vulnerability in it is being actively exploited, the spare part exclusion does nothing for you at all. The real answer is one of two things. Either a support period that runs long enough that you never hit the wall, or a migration plan with a date on it. There is no third option that involves a purchase order and a shelf. That said, the spares side and the migration side are not in conflict, and a manager should not treat them as such. Keeping critical systems running while migration is scheduled is the whole job, and an out-of-support line usually needs stocked spares precisely because it cannot be patched. Think it through from the operations side. If a controller is end-of-support, there is no firmware fix coming, so a failure of that controller is a hardware event you have to answer with hardware. The migration may be eighteen months out in the capital plan, and the line still has to run every shift in between. That means the last-time-buy question, the stock level and the sourcing route for that controller become more important, not less, in the period between the security date passing and the migration date arriving. A spare on the shelf is not a fix for the vulnerability. It is how you survive the exposure long enough to migrate away from it, which is a different and legitimate thing. There is a further reason to keep the parts route warm, and it is not about the regulation at all. A migration program takes years to execute in a plant of any size. In that window, brownfield lines break the way brownfield lines always break, at the worst possible moment, on the shift with the least cover. The plant that has a documented parts route and a sensible stock position moves through its migration without the two problems colliding. This week's checklist 1. Start the connected asset list. Get tag numbers, manufacturer, model and a rough install year for every controller, HMI, drive and I/O block that reaches the plant network. Assign one owner and set a date to have the first pass done. The support end date column can be blank for now. 2. Send a written support period question to the top five vendors or distributors by installed base. Ask for the support period end date for each product family, in month and year, in writing. Note the date you asked and put a follow-up on the calendar. 3. Name the person who owns vendor security advisories, and the backup. Confirm both can actually access the channels for your main automation brands. If not, get the subscriptions set up this week. 4. From now on, treat the support end date as a specification on new purchases, alongside I/O count and price. Add it to the standard inquiry template so it stops being an optional question. 5. Run the first triage pass: mark everything inside its support period as maintain, everything outside as migrate, and rank the migrate list by what a stop costs the line. You now have a migration queue with a security rationale behind it. 6. Put 11 December 2027 in the capital plan as a dated line item with a budget number attached, not a note. The conformity regime starts that day and it is the deadline that funds your migration queue. 7. Note the September 2026 fact in whatever risk log or plant review you run. Reporting is live, it reaches back with no age cutoff, and it is the reason your support end dates now get read as security dates. None of this is paperwork for its own sake. It is the same set of facts a maintenance manager would want anyway, which is what the equipment is, how long it will be supported, what it costs to keep running, and when it gets replaced. The regulation just put dates on the columns. If you need a fast read on what is still serviceable and what should be heading for the migration queue, the controller and drive pages at tztechio.com/plc and tztechio.com/industrial-automation are a reasonable place to check part availability against your asset list, and the brand pages for Siemens and Allen-Bradley cover most of what sits in a European legacy panel. Start with the asset list. The rest follows from it. -------------------------------------------------------------------------------------------- 🏢 About TZ Tech TZ Tech is a leading supplier of industrial automation, electrical, instrumentation, and telecommunications components. We specialize in sourcing ready-to-ship distributor stock, allowing us to offer highly competitive pricing and short lead times. Thanks to our extensive inventory, we can even source rare and discontinued parts that are hard to find elsewhere. 🛡️ Our Quality Commitment We understand that quality is your top priority. Every component undergoes a strict screening and inspection process so you can buy with absolute confidence. For legacy or discontinued parts, we believe in complete transparency and will always provide an honest, accurate report on the product's condition. Plus, all brand-new parts come backed by a full 1-year warranty. ✉️ Get in Touch Have a project or a part you need? Send us your inquiry today! Our team is dedicated to providing a fast response within 6 hours (excluding weekends).
September 14,2026
Please read on, stay posted, subscribe, and we welcome you to tell us what you think.


Sitemap | Blog | XML | Privacy Policy
In addition, with your permission, we want to place cookies to make your visit anointeraction with slOC more personal. For this we use analytical and advertisingcookies. With these cookies we and third parties can track and collect yourinternet behawior inside and outside super-instrument.com. With this we and third parties adapt super-instrument.com and advertisementsto your interest. By clicking Accept you agree to this. If you decline, we only usethe necessary cookies and you unfortunately will not receive any personalizedcontent. Please visit our Cookie policy for more information or to change yourconsent in the future.
Accept and continue Decline cookies


 +86 -17550776091


